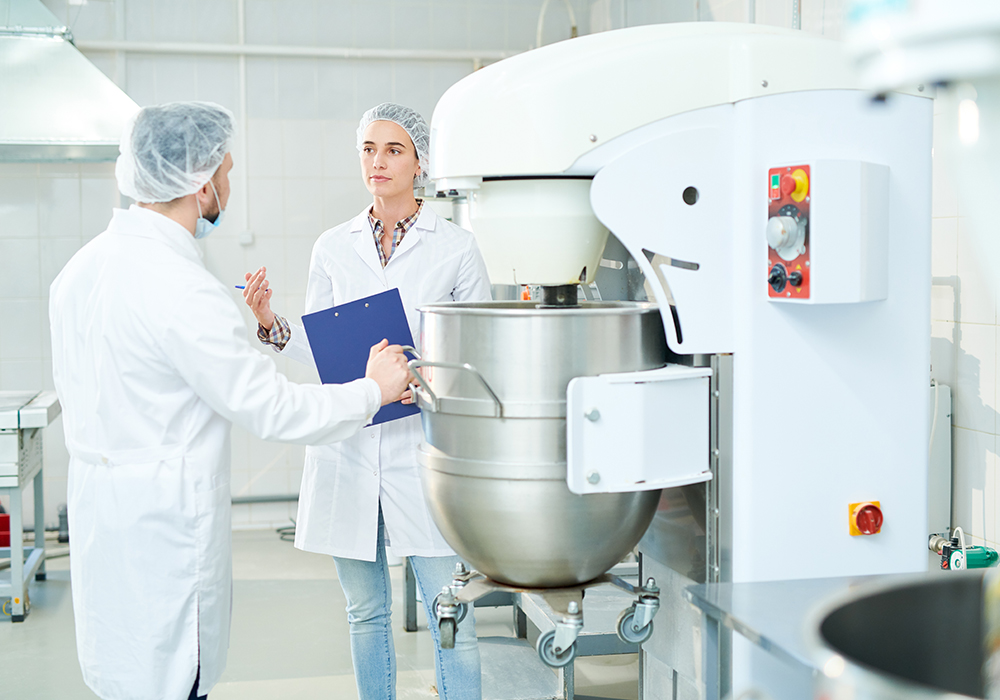
Food processing machinery product certificationIt is a process that demonstrates the compliance of these machines with certain standards in order to protect food safety and consumer health. This document offers significant advantages for both the manufacturer and the consumer.
There are different standards for food processing machines. Among the most commonly used:
Food Processing Machines Testing – Certification Period
Category: JI-JII
The hygienic design of food processing buildings and equipment has a major impact on global food safety across many sectors, from farm to fork. Poor hygienic design has led to many significant food safety problems resulting from cross-contamination of food products as a result of biological, chemical and physical hazards. Well thought out and implemented hygienic design supports food safety and product quality and contributes to the effectiveness of food safety management programmes. In 2020, the Global Food Safety Initiative (GFSI) published a set of high-level hygienic design benchmarking requirements to improve food safety from farm to fork. These Hygienic Design of Food Buildings and Processing Equipment requirements are published as scope JI (for building constructors and equipment manufacturers) and scope JII (for building and equipment users).
JI: For food building builders and processing equipment manufacturers, including the following product services and activities according to GFSI: Manufacturers of equipment for farms, food production facilities, food retail and wholesale operations, and food-specific packaging, including all components necessary to connect them together and the utilities and utensils necessary for their operation; Architects, Engineers and Designers of food processing facilities, including farm, food production, storage and retail buildings; Builders of the above facilities.
JII: For users of food making and processing equipment, including the following product services and activities according to GFSI Specification, procurement, design and construction of buildings or alterations by farmers, food manufacturers, wholesalers and retailers and packaging manufacturers for their own use; Specification, procurement, design and construction of facilities for their own use by farmers, food manufacturers, wholesalers and retailers and packaging manufacturers, and equipment, including the components necessary to interconnect them and the utilities and utensils necessary for their operation.
The structure of this white paper follows the structure of the GFSI benchmarking requirement documents JI and JII. JI: Covers requirements for the establishment of a Hygienic Design Management System for building constructors and equipment manufacturers, including hygienic design, hazard and risk management and good industry practice requirements.
JII can be viewed as hygienic design requirements for users of buildings and equipment, in addition to the scope of recognition that users of buildings and equipment will already comply with. It is about integrating hygienic design into existing Food Safety Management Systems. The method of carrying out food safety management may differ between JI and JII users: Food manufacturers are typically familiar with HACCP or HACCP-based concepts as part of Food Safety Management Systems (reference ISO 22000), where hygienic design is a prerequisite programme, whereas equipment manufacturers are typically EN 1672-2:2020, ISO 14159:2008 or is familiar with hygiene risk assessments based on other recognized standards. It is important for food safety management that expectations and interpretations of needs, capabilities and intended uses are clear when developing, implementing or transferring food premises and equipment.
In the GFSI benchmarking requirements, food is used as an umbrella term and refers to the object of each of the items covered, i.e. food, feed, packaging, as appropriate. See also abbreviations, definitions and terms. When we use the term food producer we mean users of food production buildings and processing equipment at any point in the chain from farm to fork. For suppliers of these food buildings and processing equipment, GFSI uses building constructors and equipment manufacturers.
GFSI introduced the concept of the hygienic design process. This includes the management of equipment, buildings and facilities throughout their lifecycle from the perspective of hygienic performance and compliance. The requirements are specified in various benchmarks:
Hygienic design
-Specification and design for intended use (JI:HACCP 1.9.1 or JII:HACCP 1.9.2).
-Hygienic design risk assessment (HACCP) 1.7- 1.8)
- Mitigating food safety risks with hygienic design principles (HACCP) 1.10-1.17, Good Manufacturing Practices 3.2) Hygienic Structure and Integration
-Hygienic structure and installation (HACCP) 1.14 & 1.15)
-Prevent contamination by procedures and training on using hygienic design (GMP) 4.8- 4.11; 7.2-7.3; 15.2 )
Hygienic operational use
- Cleaning, Maintenance, etc. with residual risk mitigation. ( HACCP) 1.17 )
- The use procedures and training to prevent contamination (GMP) 7.2)
- HDRA And change control Open heritage buildings/equipment ( Sorry 26 )
To confirm that hygienic assets (building/equipment) will meet all hygienic design requirements specified criteria, their compliance will be assessed at various stages throughout the design and commercialization phases and during use.
Workarounds for compatibility, design changes, and handling deviations from design criteria should be documented and records kept at the manufacturing facility where the hygienic asset is used.
Non-assigned assets, typically equipment modules or units integrated into lines, should be risk assessed by the supplier against the intended range of products and processes to confirm suitability in principle for a particular application (e.g. for dry foodstuffs). Compliance with hygienic design and criteria for cleanliness can be verified by certification according to Astor Mayer procedures. Evaluate Hygienic design based on EN ISO 14159 and/or EN 1672-2 should be applied.
The characteristics and (expected) outcomes of the qualification process can be used to establish concrete agreements between the supplier and the customer during the purchasing process.
Depending on which stage of the life cycle assessment you are in, activities related to hygienic design will be as follows:
design phase
Concepts or feasibility studies often result in the establishment of user or stakeholder requirements. These requirements should be specified in one or more documents to be reviewed. In the absence of user requirements specification (unassigned entities), designers, focus groups, consultants, customer surveys, customer partnerships, co-development with customers, etc. may have to use other resources to determine user requirements, such as
Based on an approved requirements specification, functional and design specifications should be developed to translate the requirements into detailed design solutions (for less complex assets this may be a single step). In an iterative process often referred to as design qualification, design solutions must be reviewed before a "design freeze" and agreement on fabrication of an asset is reached. A hygienic design risk assessment (HDRA) should be carried out as part of the design qualification process. Based on the outcome of this HDRA, purchase specifications can also be determined. These specifications can determine details regarding hygienic design.
Installation and commissioning phase
During installation, it must be checked that the correct hygiene product has been purchased and that it has been installed in accordance with the approved design specification.
After installation and before use on the user's premises, it must be verified that all functional (operating) parameters, limits and tolerances detailed in the user requirements specification can be met to achieve the required hygienic performance. Once the equipment/building components are installed at the user's site, a site acceptance test (SAT) must be performed and usually includes functional testing.
Using Operational
Documentary evidence should be provided through verification (hygiene-related process adequacy) to confirm that new hygienic assets consistently perform according to the criteria set out in the user requirements specifications, including aspects of food safety, quality and cleanability.
Older establishments whose hygienic performance has not previously been assessed should be subject to hygienic design risk assessments and retrospective cleaning verifications based on historical data.
Continuous and appropriate planning should be carried out for the periodic verification of the hygienic performance, operational use and maintenance of all hygienic facilities throughout their lifetime.
- EN 1672-2:2020 Food processing machinery - Basic concepts - Part 2: Hygiene and cleanability requirements
- ISO 14159:2008 Safety of machinery - Hygiene requirements for the design of machinery
Equipment manufacturers have the responsibility to inform users of food safety risks that cannot be eliminated by hygienic design and also to provide the equipment user with an operating manual containing the information required for the hygienically safe operation of the relevant equipment within the limits of use. These include but are not limited to:
- Limitations And operational uses
- Technical quantity (e.g. control or monitoring (devices)
- Inspection for disassembly, cleaning and maintenance
- Cleaning
Testing – Certification Period
1. Scope
1.1 The evaluation and testing of equipment intended for certification submitted to ASTOR MAYER covers a wide range of ASTOR MAYER Guidelines, individual designs and manufacturing features that are specific to the item being evaluated.
ASTOR MAYER maintains documentation of all elements important to the interpretation, evaluation and certification process, in addition to published guidelines to ensure uniformity between Authorized Equipment Evaluators (AEO), Authorized Testing Laboratories (ATL) and the Certification Officer.
1.2 This document is publicly available on the ASTOR MAYER website for easy access. The decisions documented in section 5 are being considered for inclusion in planned updates of the relevant guidelines to ensure transparency and maintain the guidelines with the most current information available for certification.
2. Authority
2.1 The development and maintenance of this document is the responsibility of the Working Group Certification with the assistance of the Certification Officer and under the authority of the Product Certification Directorate. The Working Group consists of experts who make decisions about when specific evaluation, testing, and certification techniques are necessary to ensure uniform evaluations.
2.2 This document has been published by the Certification Officer on the website ASTOR MAYER. https://www.astormayer.com.tr is kept.
3. Structure
3.1 This document is maintained as an MSWord document, which is also converted to Acrobat .PDF format for distribution and publication on the website.
3.2 Reference Documents
EN ISO 14159:2008 Safety of machinery - Hygiene requirements for the design of machinery (ISO 14159:2002)
EN 453:2014 Food processing machinery - Dough mixers - Safety and hygiene requirements
EN 454:2014 Food processing machinery - Planetary mixers - Safety and hygiene requirements
EN 1672-2:2005+A1:2009 Food processing machinery - Basic concepts - Part 2: Hygiene requirements
EN 1673:2000+A1:2009 Food processing machinery - Rotary rack ovens - Safety and hygiene requirements
EN 1674:2015 Food processing machinery - Dough sheeters - Safety and hygiene requirements
EN 1678:1998+A1:2010 Food processing machinery - Vegetable cutting machines - Safety and hygiene requirements
EN 1974:2020 Food processing machinery - Slicing machines - Safety and hygiene requirements
EN 12041:2014 Food processing machinery - Moulders - Safety and hygiene requirements
EN 12042:2014 Food processing machinery - Automatic dough dividers - Safety and hygiene requirements
EN 12043:2014 Food processing machinery - Intermediate provers - Safety and hygiene requirements
EN 12267:2003+A1:2010 Food processing machinery - Circular saw machines - Safety and hygiene requirements
EN 12268:2014 Food processing machinery - Band saw machines - Safety and hygiene requirements
EN 12331:2021 Food processing machinery - Mincing machines - Safety and hygiene requirements
EN 12355:2022 Food processing machinery - Derinding-, skinning- and membrane removal machines - Safety and hygiene requirements
EN 12463:2004+A1:2011 Food processing machinery - Filling machines and auxiliary machines - Safety and hygiene requirements
EN 12505:2000+A1:2009 Food processing machinery - Centrifugal machines for processing edible oils and fats - Safety and hygiene requirements
EN 12851:2005+A1:2010 Food processing machinery - Catering attachments for machines having an auxiliary drive hub - Safety and hygiene requirements
EN 12852:2001+A1:2010 Food processing machinery - Food processors and blenders - Safety and hygiene requirements
EN 12853:2001+A1:2010/AC:2010 Food processing machinery - Hand-held blenders and whisks - Safety and hygiene requirements
EN 12854:2003+A1:2010 Food processing machinery - Beam mixers - Safety and hygiene requirements
EN 12855:2003+A1:2010 Food processing machinery - Rotating bowl cutters - Safety and hygiene requirements
EN 12984:2005+A1:2010 Food processing machinery - Portable and/or hand-guided machines and appliances with mechanically driven cutting tools - Safety and hygiene requirements
EN 13208:2003+A1:2010 Food processing machinery - Vegetable peelers - Safety and hygiene requirements
EN 13288:2005+A1:2009 Food processing machinery - Bowl lifting and tilting machines - Safety and hygiene requirements
EN 13289:2001+A1:2013 Pastry processing plants - Dryers and coolers - Safety and hygiene requirements
EN 13378:2001+A1:2013 Pasta processing plants - Pasta presses - Safety and hygiene requirements
EN 13379:2001+A1:2013 Pasta processing plants - Spreader, stripping and cutting machine, stick return conveyor, stick magazine - Safety and hygiene requirements
EN 13389:2005+A1:2009 Food processing machinery - Mixers with horizontal shafts - Safety and hygiene requirements
EN 13390:2002+A1:2009 Food processing machinery - Pie and tart machines - Safety and hygiene requirements
EN 13534:2006+A1:2010 Food processing machinery - Curing injection machines - Safety and hygiene requirements
EN 13570:2005+A1:2010 Food processing machinery - Mixing machines - Safety and hygiene requirements
EN 13591:2005+A1:2009 Food processing machinery - Fixed deck oven loaders - Safety and hygiene requirements
EN 13621:2004+A1:2010 Food processing machinery - Salad dryers - Safety and hygiene requirements
EN 13732:2002+A2:2009 Food processing machinery - Bulk Milk Coolers on Farms - Requirements for construction, performance, suitability for use, safety and hygiene
EN 13732:2022 Food processing machinery - Bulk milk coolers on farms - Requirements for performance, safety and hygiene
EN 13870:2015 Food processing machinery - Portion cutting machines - Safety and hygiene requirements
EN 13870:2015+A1:2021 Food processing machinery - Portion cutting machines - Safety and hygiene requirements
EN 13871:2014 Food processing machinery - Cubes cutting machinery - Safety and hygiene requirements
EN 13885:2022 Food processing machinery - Clipping machines - Safety and hygiene requirements
EN 13886:2005+A1:2010 Food processing machinery - Cooking kettles equipped with powered stirrer and/or mixer - Safety and hygiene requirements
EN 13951:2003+A1:2008 Liquid pumps - Safety requirements - Agrifoodstuffs equipment - Design rules to ensure hygiene in use
EN 13951:2012 Liquid pumps - Safety requirements - Agrifoodstuffs equipment; Design rules to ensure hygiene in use
EN 13954:2005+A1:2010 Food processing machinery - Bread slicers - Safety and hygiene requirements
EN 14655:2005+A1:2010 Food processing machinery - Baguette slicers - Safety and hygiene requirements
EN 14957:2006+A1:2010 Food processing machinery - Dishwashing machines with conveyor - Safety and hygiene requirements
EN 14958:2006+A1:2009 Food processing machinery - Machinery for grinding and processing flour and semolina - Safety and hygiene requirements
EN 15166:2008 Food processing machinery - Automatic back splitting machines of butchery carcases - Safety and hygiene requirements
EN 15774:2010 Food processing machinery - Machines for processing fresh and filled pasta (tagliatelle, cannelloni, ravioli, tortellini, orecchiette and gnocchi) - Safety and hygiene requirements
EN 15861:2012 Food processing machinery - Smokehouses - Safety and hygiene requirements
EN 16743:2016 Food processing machinery - Automatic industrial slicing machines - Safety and hygiene requirements
• other ASTOR MAYER Documents deemed appropriate
3.3 Procedures
3.3.1 Specific conditions that experts have determined should be documented in the testing procedure are given below.
- This includes procedures for testing specific pieces of equipment, exclusion of tests, and
- ASTOR MAYER Includes unreleased changes related to the testing and certification process.
These changes are made taking into account the revisions made to the standards given in the reference documents.
4. Updating Requirements in the Guides
The Chair of the WG responsible for the preparation of a ASTOR MAYER Guide in which a requirement of this document will be incorporated will consult with the WG to ensure the accuracy of the reference in the specified guide.
After final approval of the guidance, the WG will reissue this document without the requirement included in the currently published guidance.
5. Requirements
5.1 Additional requirements for design
5.1.1 Mechanical force seals
When an elastomeric seal is pressed into a specially shaped groove machined into a one-piece component, the seal must completely fill the groove. Expansion/contraction of the gasket will only be possible in the product contact area and it must be ensured that the gasket provides a crack-free joint at the product contact interface under the intended conditions of use. Finite Element Analysis provided by the customer can be used as a tool for verification in conjunction with mandatory cleanability testing. This type of mechanical force seal is not intended for routine disassembly for cleaning and the manufacturer must provide routine inspection and replacement instructions to ensure hygienic integrity is maintained.
5.1.2 O-ring groove design
Single flat face O-ring connections are acceptable for cleanability testing only if technical or functional reasons justify it.
Doc. Square gutters designed to 3-A requirements are acceptable if the 2 test indicates easy cleanability. O-rings for sliding seals are unacceptable: except for the valve disc seal of a mixture-tight valve that has been subjected to the mandatory cleanability test according to document 2.
5.1.3 shrink-fit / press-fit (metal to metal/metal to ceramic)
Press-fits using metal-to-metal components are not permitted according to document 2. 8. Press-fits made using plastic and metal must be tested according to document 2.
Shrink-fit can be used to join similar or dissimilar materials and the assembly must be tested according to document 2.
5.2 Testing of equipment
This section is about testing requirements and procedures for specific equipment and their implications for certification.
5.2.1 Different equipment sizes
The result of the cleanability test can be transferred to other dimensions of the equipment as long as their geometries are similar. The worst case dimension should be tested for cleanability. Customer-supplied computational fluid dynamics (CFD) simulation can be used to select the worst-case size on equipment without rotating parts during cleaning (e.g., not for pumps). Flow rate and wall shear stress are the information needed to find the worst cleanable dimension of the equipment to be tested. The CFD calculation should be performed in a steady state with water at 1.5 m/s and ambient temperature. The CFD calculation must take into account that the inlet is relative to the reference pipe diameter or a pipe diameter according to a pipe standard (for example, reducers must be included).
In the following sections, additional specific criteria for the selection of the worst case are specified.
A consensus needs to be reached between the customer and the Working Group to determine the worst case and therefore decide on the size and configuration to test.
5.2.2 Additional requirements for testing
5.2.2.1 Elastomeric material testing, including false positive results
The behavior of different elastomeric materials and recipes in the same groove design of connecting parts can affect cleanability, so only tested materials can be certified.
The tested materials are specified in the test report and evaluation report.
Testing for pH change due to acid leaching may be necessary to identify false positive results, especially in the doc.2 test with silicone. For this evaluation, the material is incubated in agar at 58 ºC without microorganisms.
5.2.2.2 valves
Valves are normally tested in all flow directions. When a specific flow direction is mentioned in the user manual and/or a flow arrow is marked on the outside of the valve body, valves can only be tested and certified for that direction.
A 45° stem is different in geometry from a 90°/180° stem and should be tested independently.
Worst case determination:
- Worst case for different bodies: double-body valve (LL body) is considered the worst case compared to single-body valve (L body). Split flow (T-body or diverter valve) cannot be tested. In this case, the manual should specify how to purge (full flow through the valve by closing an outlet) and the test should be conducted accordingly.
- Worst case for different sizes with similar geometry: As an alternative to the CFD option mentioned in Section 4.1, the worst case can be determined by the Kv value: Take the Kv value (m3/h) and divide it by the flow rate required to achieve a velocity of 1.5 m/s at the valve inlet -> the highest ratio number determines the worst case size.
- In some cases where geometry changes (e.g. plug design), CFD simulation may be the most appropriate way to determine the worst case.
5.2.2.2.1 sample valve
During the cleaning step of the cleanability test, all one or two outlet sample valves must be opened to drain or return to the cleaning tank. The flow at the outlet depends on the back pressure of the reference pipe and the main pipe. This should be 1 bar.
5.2.2.2.2 butterfly valve
Large steps in the seal in the shaft sealing area are not allowed. Worst case detection:
As an alternative to CFD, it is possible to calculate the flow field in the middle of the valve. The worst case will be the one with the largest area compared to the pipe diameter.
5.2.2.2.3 seat valve (L-shaped body)
Seat valves with L-shaped bodies must be cleaned in both directions (if they are intended to be certified for both flow directions).
5.2.2.2.4 diverter valve
All possible flow directions should be tested separately. It is not necessary to split the flow.
Worst case detection:
Worst case if 3 bodies are together.
5.2.2.2.5 double seat mixture proof valve
These valves with 4 ports should be tested as follows:
- create a pipeline loop that will pass through both casings, lowering it first to remove air
- only one flow path to examine (3 tests)
- fouling with the valve open (main stroke), operate (close) the valve several times during the fouling step
- clean in closed position with seat lift; number of seat lifts according to the manual
- filling with agar and incubation in closed position
- pay attention to a straight, unobstructed inlet section in the pipeline loop
Worst case detection:
Maximum leakage flow (during seat lift) compared to inlet flow through the valve.
5.2.2.2.6 dosing valves (filling machines)
A CIP circuit must be created to test the valve. Reference the pipe to the valve inlet diameter and reference the worst case to the lowest velocity at the valve. Contamination: Install CIP return connection and pump/dose sour milk into cycle Drying: Disconnect CIP return connection, clean and sterilize; dry the unit in the open position
Cleaning: insert the sterile CIP return connection, then clean the loop
5.2.2.2.7 vent valve to atmosphere
A relief valve shall be tested on the product contact side only. The atmospheric side is not included. It must be possible to actively open the valve. Contamination with valve action, cleaning with open valve, incubation with closed valve.
5.2.2.3 pumps
In dynamic situations the “static” CFD of the pumps is not important. Smaller or larger sizes may be certified if the design review concludes that they are geometrically equivalent/scalable.
Cleaning instruction: A speed controller must be used to achieve 1.5 m/s and a minimum back pressure of 1 bar in the reference pipe. It is possible for the manufacturer to specify a higher back pressure during cleaning if this is stated in the cleaning instructions. This back pressure should be used during the testing program.
5.2.2.3.1 peristaltic pump
To perform the test, the pump can only be dried if the cylinders are removed or moved away from the hose and air can flow through the hose. If this is not possible, the pump cannot be tested.
5.2.2.3.2 centrifugal pump
Drain valve:
If a pump has a drain port, the valve should be tested along with the pump. For Class I certification the relief valve must be automatic.
Test procedure: only the seating area of the valve is soiled (closed and not operated during soiling and drying), pulsed during cleaning. There should be a statement in the manual stating that the valve should be used only as a relief valve and not as a sampling valve.
Exception: the drain valve is also used as a sampling valve: The valve must be operated in the fully open position during fouling, drying and cleaning.
Worst case detection:
Worst case: choosing the least efficient impeller and having the smallest ratio of inlet pipe diameter to casing diameter
5.2.2.3.3 screw pump
Test only one direction (flow direction towards the mechanical seal), even if the pump is used in both directions. Worst case detection: selecting the screw with the smallest ratio of inlet pipe cross-section to casing cross-section and a slope that gives the slowest speed of 1.5 m/s per minute
5.2.2.3.4 lobe pump
Worst case detection:
Primary criterion: lowest rotation speed to reach 1.5 m/s at at least 1 bar back pressure.
Additional criterion: minimum shear flow relative to theoretical displacement per revolution at recommended back pressure for cleaning
If certain sizes in a pump series cannot reach 1.5 m/s and require a booster pump, the worst case is selected from sizes that do not need a booster pump. For certification of smaller sizes, the cleaning instruction must specify the use of a booster pump and/or bypass loop to obtain the flow required to clean the reference pipe.
5.2.2.3.5 progressive cavity pump
Pumps with and without a bypass port are considered two different versions and both should be tested. Worst case detection:
Minimum ratio of inlet pipe diameter to body diameter;
Pump without bypass: rotor with slowest RPM to reach 1.5 m/s
5.2.2.3.6 row mixer
Worst case detection:
Worst case: Choosing the least efficient pump with the smallest ratio of inlet pipe diameter to casing diameter
diaphragm pump
Drainability is required. It can be achieved with magnetic ball valves to open the pipeline or with a system that allows rotation to connect the pump to the process using hoses.
The reference pipe diameter is selected according to the single inlet diameter of the pump.
An additional centrifugal pump (booster pump) can be used to achieve the required speed of 1.5 m/s from the pump inlet.
Worst case detection:
The lowest flow rate in the pump; Size selection for testing may be based on the largest ratio of aperture to port size (i.e., largest aperture/smallest port size).
5.2.2.3.8 blower pump
Worst case detection:
If cleaning is done without rotation: static CFD is accepted.
If rotating cleaning: the largest gap between the blower and the inlet body with the lowest revolutions per minute. 5.2.2.4 sensors
Sensors must be tested in the configuration according to ASTOR MAYER Position Paper “Easy-to-clean pipe connections and pipe connections”. The process connection (gasket) is not considered as long as it is a connection listed in the Position Paper. If a T-piece is used for testing, it must have the same diameter in the same branch (sensor adapter) as the main pipe.
The T-piece used (branch T at 90°) must have maximum L according to the criterion L < (D-d). Sensors (those that are very long for basic functional reasons) can be tested in a tee with the sensor branch parallel to the flow.
5.2.2.4.1 temperature sensors
Temperature sensors manufactured inside the thermowell do not need to be tested if all Hygienic Design Criteria are met. 5.2.2.4.2 pressure sensors, diaphragm/inline
Laser welded diaphragm type pressure sensors are accepted without testing as long as the weld seam is smooth and free of visible defects.
Internal radii at the bends of the diaphragm do not require a 3 mm radius if the maximum peak-to-valley dimension within the profile does not exceed 0.8 mm.
5.2.2.4.3 magnetic inductive flow meter
Worst case detection:
If the size of the electrodes is the same across the size range of the flowmeter, a smaller flowmeter diameter is the worst case due to the ratio between the electrode surface and the radius of the pipe.
In the case of different sizes of the electrode, the worst case is the largest size electrode in the smallest diameter pipe.
The intersection angle around the electrodes should be checked.
5.2.2.4.4 Coriolis flow meter
Radius on bends is not a scalability issue. The pipe needs to be cut to check the surface roughness.
Worst case detection:
Double-pipe meters: check all dimensions and select worst case based on CFD for separator design at inlet and outlet. 5.2.2.5 tank cleaning device
Dock. According to 2, the tank cleaning device should rotate during contamination. E.g.:
- single-component rotator: the fouling section can be shaken to move the device
- gear driven rotary cleaning devices: soil can be pumped to rotate the device or the device can be rotated remotely.
Cleaning parameters (flow rate, pressure) must comply with the specifications (minimum parameters) in the cleaning instructions. The diameter of the reference pipe will be selected according to this flow rate.
When a tank cleaning device is installed using a stainless steel R clip (spring), there must be clearance between all surfaces when installed. Therefore, this is not considered a metal-to-metal connection.
5.2.2.6 tank flanges for explosion vents
The sealing design of a tank flange can be tested as a cross-sectional piece supplied by the customer and installed in a pipeline to evaluate cleanability.
Example of test configuration: Only the product side of the seal arrangement is evaluated.
5.2.2.7 tube heat exchanger
Spiral heat exchanger tubes, options:
a) seamless extruded -> visual inspection and roughness control, no cleanability test required
b) longitudinally welded -> inspection and roughness check, no cleanability test required
Drainability: If multiple straight tube heat exchangers are installed with return loops in horizontal stacks and are not completely self-draining, pressurized clean gas can be used to remove residual water and dry the surfaces. This should be stated in the cleaning instructions.
Worst case detection:
Multi-pipe heat exchanger: The diameter of the inlet pipe is used to select the size of the reference pipe.
The worst case would be the unit giving the slowest speed on the inner tubes.
If this can be achieved with different configurations, the worst case will be the one with the highest ratio of the area of the distribution plate to the available flow area through the tubes (distribution plate).
5.2.3 Additional requirements for testing
5.2.3.1 fully welded equipment
If a piece of equipment is fully welded and there is no connection where bacteria can enter the product contact area, there is no need to perform a bacteria leak test.
5.2.3.2 gasket without access
Sensor: seal at the front, but the empty space behind (electronics) should be tested for bacterial tightness by filling the internal sensor with bacteria.
5.2.3.3 double mechanical seal
The double mechanical seal must be in working order and the environment must be washed with sterile water. Contamination will be applied to the atmospheric side of the seal.
Easy to Clean Pipe Connections and Process Connections
When integrating hygienic process components or equipment into a production line, it is crucial to ensure that these elements are connected in a way that not only maintains hygiene but also facilitates easy cleaning. This approach is important to maintain process integrity and ensure product safety. Process connections or pipe connections of good hygienic and easily cleanable design are specified in accordance with the ASTOR MAYER Guidelines (Hygienic Design Principles), (Equipment in Closed Processes), (Pipe Joints) and (Elastomeric Seals) and their in-situ cleaning performance can be evaluated in accordance with the ASTOR MAYER Guidelines.
Critical aspects to design and connectivity include:
• preventing cracks or protrusions of the gasket larger than 0.2 mm,
• providing an axial stop by controlled compression of the seal and
• a means for centering flanges.
This list is not comprehensive and may be subject to revision at any time. If additional connections have been successfully tested for site cleanability, they can be used and added to the list below. It is important to avoid dead legs when installing equipment or sensor parts with process connections for liquid food processing in enclosed equipment.
pipeline connection
In pipelines, the length of the dead leg should be less than the inner diameter of the dead leg. If the sensor projects towards the dead leg, the length (L) of the dead leg must be L ≤ (D - d). The relative diameter d of the sensor will vary depending on the design.
If the calculation of L/(D - d) for a given connection size results in a ratio greater than 1, this size does not meet the certification requirements and is excluded from the size range considered for ASTOR MAYER certification.
The routing should allow for self-draining of liquids and promote the evacuation of air to prevent the accumulation of air bubbles.
tank connection
Sensors mounted on tanks must be flush with the inside of the tank wall. If there is a dead leg for technical reasons, it must be ensured that the spray from the cleaning device can reach all surfaces. The above criteria L ≤ (D - d) still apply.
Pipe connections
DIN 11853-1:2017, Hygienic screw pipe connection with O-ring
DIN 11853-2:2017, Hygienic flange pipe connection with O-ring
DIN 11853-3:2017, hygienic clamp pipe connection with O-ring
DIN 11864-1:2017, Aseptic screw pipe connection with O-ring
DIN 11864-2:2017, Aseptic flanged pipe connection with O-ring
DIN 11864-3:2017, Aseptic clamp pipe connection with O-ring
DIN 11851 with riser seals
 Türkçe
 English